HS Code Lookup for Heading 8455
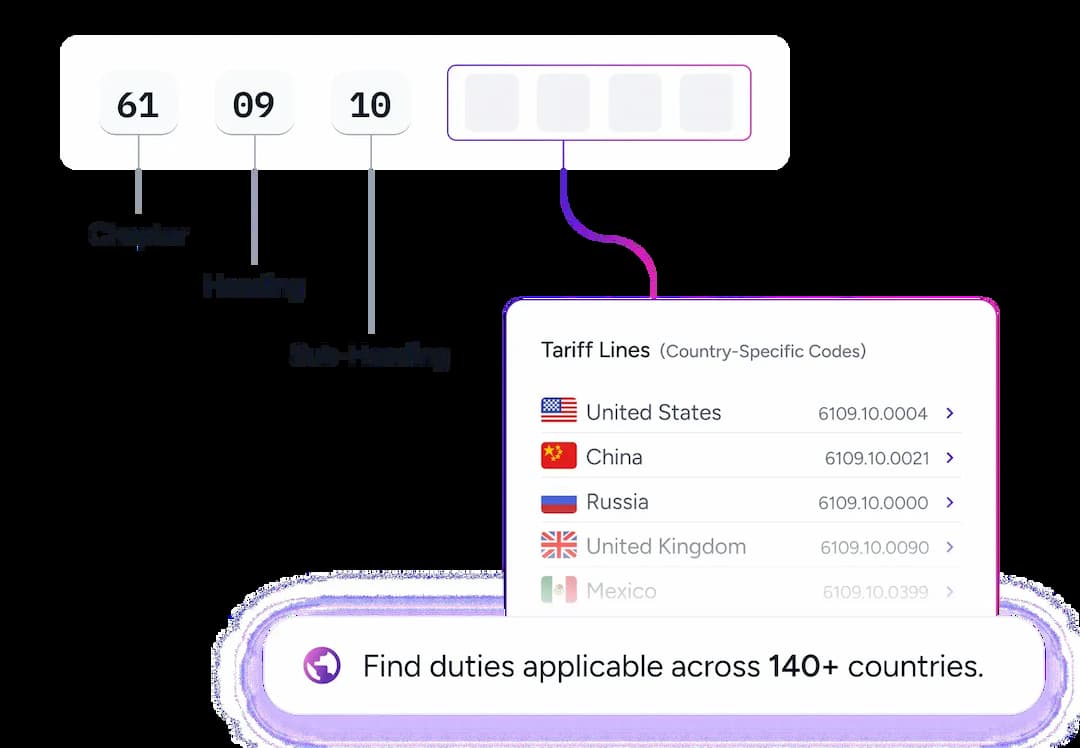
HS Code Lookup helps classify products under appropriate HS code and find duties applicable across 140+ countries. Find and discover HS classification, tariffs, taxes, controls, rulings, ECCNs, and default and preferential duties for HS code 8455.

WCO Notes for Heading 8455
84.55 ‑ Metal‑rolling mills and rolls therefor.
8455.10 ‑ Tube mills
‑ Other rolling mills :
8455.21 ‑ ‑ Hot or combination hot and cold
8455.22 ‑ ‑ Cold
8455.30 ‑ Rolls for rolling mills
8455.90 ‑ Other parts
(I) ROLLING MILLS
Rolling mills are metal working machines consisting essentially of a system of rollers between which the metal is passed; the metal is rolled out or shaped by the pressure exerted by the rollers, and at the same time the rolling modifies the structure of the metal and improves its quality. In some cases, in addition to their normal functions, rolling mills may be used to produce a pattern on the metal surface, or to roll together two or more sheets of different metals to produce a laminated product.
Similar machines for rolling materials other than metal, e.g., calenders, are excluded (heading 84.20). Other roller machines (e.g., for gumming metal foil on to a paper support) (heading 84.20), bending, folding, straightening or flattening machines (heading 84.62) are not regarded as rolling mills in the sense described above and are therefore also excluded from this heading.
Rolling mills are of various types according to the particular rolling operations for which they are designed, viz. :
(A) Rolling out to reduce the thickness with a corresponding increase in length (e.g., in the rolling of ingots into blooms, billets or slabs; rolling of slabs into sheet, strip, etc.).
(B) Rolling of blooms, billets, etc., to form a particular cross‑section (e.g., in the production of bars, rods, angles, shapes, sections, girders, railway rails).
(C) Rolling tubes.
(D) Rolling of wheel blanks or wheel rim blanks (e.g., to shape the flanges of railway wheels).
Most rolling mills are designed for the operations indicated at (A) or (B) above. The essential element of these is known as a “stand”, and consists of two, three or four rolls mounted horizontally one above the other in heavy metal housings, the metal being passed through an adjustable gap between the rollers. In three high and double two high stands, the metal, after being passed between two of the rollers, is then passed through two others; some stands have two or more additional rolls which act as support to give additional power and steadiness to the working rollers.
Most mills consist of a number of such stands arranged either side by side, or slightly staggered, or tandem fashion (for example, continuous rolling mills for sheets); the speeds and gaps of the rollers are adjusted to produce a progressive and gradual rolling down of the metal.
Certain rolling mills may have side rollers for working on the edges of the material, or for producing particular sections (e.g., girders).
For flat products (slabs, sheet, strip, etc.) the rollers are plain (except that certain finishing rollers may produce a simple ridged pattern). In many cases (e.g., for the operations under (B) above) the rolling is not done over the full width of the rolls, but the working rollers have channels cut in their surface so that a gap (or pass) of a particular shape is formed between the two rollers. The metal as it passes through is formed to the shape of the gap, and passing through a succession of such gaps, gradually varying in shape, the metal is thus worked to the desired cross‑section.
Rolling mills of the kinds referred to above vary considerably in size, from small machines for rolling precious metals up to very heavy rolling mills for steel.
Most of the rolling mills referred to above are for hot rolling, but certain finishing mills (particularly for sheet or strip) roll the metal cold.
Among the rolling mills of the type referred to at (C) and (D) above are :
(1) Mannesmann or similar machines for piercing billets; these have large inclined rollers which rotate the heated billet and force it over a piercing mandrel, thus forming the rough tube.
(2) Mills for rolling out the pierced billets to reduce the thickness of the walls, increase the length and produce a satisfactory surface to the walls. The walls of the tube are worked between a mandrel or plug on the inside, and either rollers with a circular pass or conical rollers on the outside. In certain cases rollers with eccentrically cut channels to give a variable pass are used (step rolling).
(3) Finishing mills for tubes, to finish or reduce the thickness of the walls, or to reduce the diameter, or produce a perfect circular cross‑section. These may operate with or without an internal mandrel.
(4) Radial mills for rolling the walls of large diameter cast steel tubes. The tube rotates between a number of rollers operating on the outside and corresponding rollers on the inside.
(5) Wheel or disc rolling mills. These usually consist of sets of conical or cylindrical rollers variouslyarranged, between which the roughly formed wheel revolves; the various parts of the wheel (e.g., flanges of railway wheels) are worked to the required shape by the pressure of the rollers. Similar machines are used for shaping flanged tyres for railway wheels, and for certain railway rails.
In general, the operation of rolling mills requires a large amount of auxiliary equipment such as guides, roller tables, handling equipment, re‑heating furnaces, pickling tanks, strip coilers, shears and saws, cooling beds, weighing or marking machines, straightening or flattening machines, control apparatus (mechanical, electric or electronic), etc.
(II) ROLLS AND OTHER PARTS
Subject to the general provisions regarding the classification of parts (see the General Explanatory Note to Section XVI), the heading covers parts of rolling mills. Among the parts covered by this heading are the rolls of rolling mills. These vary considerably in length and diameter, those for steel ranging approximately from 30 to 520 cm in length and from 18 to 137 cm in diameter. They are made of cast iron, or of cast or forged steel, usually specially hardened on the surface and carefully machined to exact dimensions; they may be plain, or with grooves of various shapes to form the necessary passes. Each roll ends in necks, often specially shaped for mounting in the housings of the rolling mill. Outside the roll necks, wobbler‑ends are cut to which the driving force is applied.

What is HS code 8455?

How many sub-headings are there in HS code 8455?
International Trade Compliance Simplified